Squishy Returns: Physics, Not Marketing
- Share
- publisher
- Chloe
- Issue Time
- Sep 23,2026
Summary
The 5 physical failure modes behind squishy toy returns — recovery drift, oil bleed, filling clumps, seam failures, carton crush — plus 7 questions to filter suppliers.
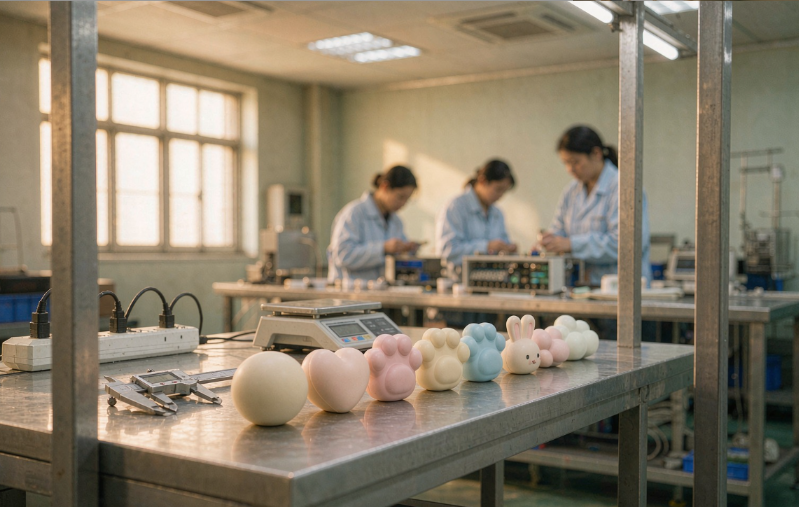
Squishy Returns: Physics, Not Marketing
A factory-side breakdown of the five real reasons slow-rising squeeze toys come back — and the seven questions that separate a good supplier from a cheap one.
Every month, a brand owner sends us the same email, usually with screenshots attached:
"Sales were fine. Reviews were not. 'Went hard in two weeks.' 'Sticky surface.' 'Smells weird.' 'Doesn't look like the video.' Return rate is at 11% and climbing. What are we doing wrong on the marketing side?"
Nothing. The marketing is fine. The compound is not.
Almost every squeeze-toy return traces back to one of five physical failure modes that are decided at the compounding table — months before anyone writes an ad. Suppliers don't volunteer these, because explaining them means explaining what they skipped. So we will.
1. Slow-rising becomes dead-rising
A slow-rising squeeze toy is graded by recovery time — how long the shape takes to come back after a squeeze. Around 8 seconds is the sweet spot: slow enough to feel satisfying, fast enough to feel alive.
Here's the part nobody puts in a quotation: recovery time is a moving target. The cheap way to hit a low unit price is to load the TPR compound with mineral filler. Filler is cheap; softener is not. A ball heavy on filler can leave the factory at a respectable 8–10 seconds — and then a hot ocean container and a humid warehouse finish the job. Three weeks later it recovers in 25 seconds, or worse, it slowly sags and never fully comes back.
The customer never writes "the recovery time drifted." They write "it feels dead." And they return it.
Ask for the recovery time spec at day 30, not at shipment. In writing.
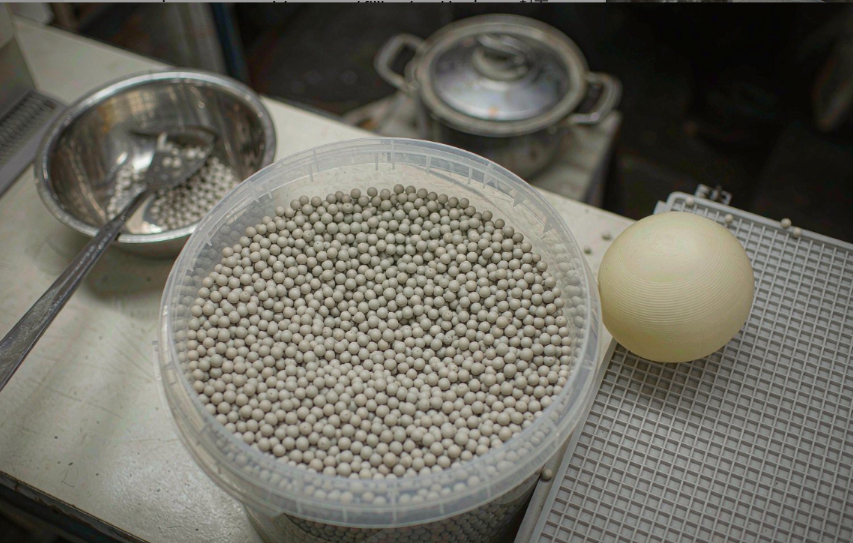
2. Oil bleed: the "sticky" complaint
Same root cause, second symptom. When a compound is over-filled and under-softened in the right (wrong) way, unbound oil migrates to the surface over time. The toy arrives slightly greasy, attracts dust and hair within days, and can even stick to its own poly bag.
In your listing photos, it looks perfect. In the customer's hand, it feels cheap — and that gap between photo and touch is exactly what "looks nothing like the video" reviews are made of.
If a factory has never heard of a heat-aging test for oil bleed, they're not testing for it. Which means they're shipping it.
3. The filling fails before the skin does
The classic flour fill is a beautiful thing: dense, silent, evenly slow. It is also hygroscopic — flour absorbs moisture. If the fill port or the molding seam isn't properly sealed, humidity works its way in and the filling starts to clump. The squeeze goes from smooth to lumpy, and in bad cases a faint sour smell develops.
Syrup-based fills have the opposite failure mode: heat. Inside a summer container, internal temperatures can pass 60°C. A fill that flows nicely at room temperature migrates to one end of the toy in transit, and the customer receives something that squeezes like a half-full water bottle.
Both fillings can be excellent. Both fail for predictable, testable reasons. The difference between factories is whether anyone actually tests for it.
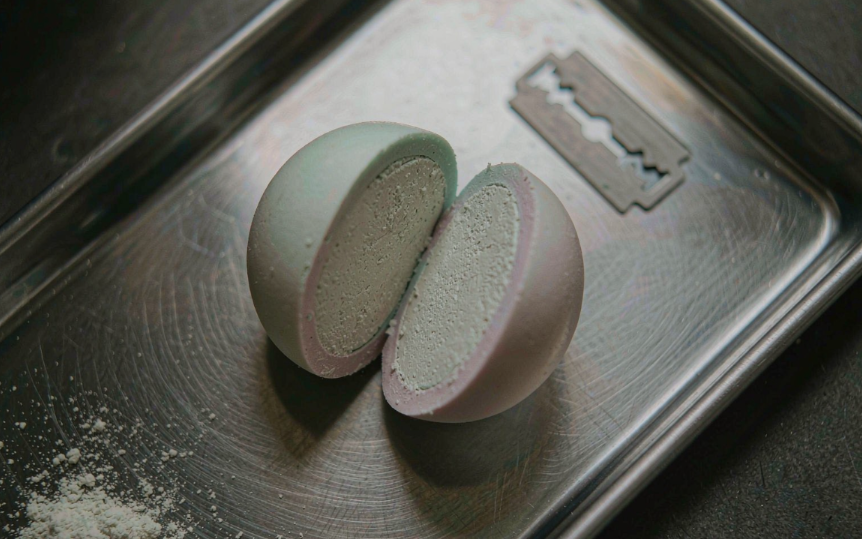
4. Seams and attached parts: the complaint that isn't a return
Glued-on eyes, stitched patches, hard-plastic details on a soft body — two materials with different thermal expansion rates joined by one drop of adhesive.
It survives QC at a comfortable 22°C. It does not survive a container at 65°C, or a kid's backpack. And when an eye pops off, the customer doesn't file a return — they file a safety complaint. That's a much more expensive conversation.
Any attached part should pass a pull test after heat aging, not before.
5. Packaging crush: the most preventable return
Squeeze toys ship soft. Stack three cartons of them and the bottom layer arrives as discs. Nobody returns a product for being "slightly flattened" — they return it because your listing photo promised a plump, proud little shape and the box delivered a pancake.
This is the cheapest failure mode on the list to fix — carton dimensions, layer pads, void fill — and somehow the most common.
Why you can't fix this with marketing
You can A/B test your way to better click-through. You cannot copywrite your way out of oil bleed. A return caused by physics is fixed at the compounding table — by your supplier, or not at all
The 7 questions to send before you place a PO
Copy these into your next supplier email. A good factory will answer all seven without flinching. A cheap one will answer two and change the subject.
1. What is the guaranteed recovery time at day 30, not at shipment — and will you put it in the spec sheet?
2. What is the filler load in your TPR compound, and what softener system do you use?
3. Do you run a heat-aging test for surface oil bleed? At what temperature and duration?
4. What fill do you use, and how is it sealed against humidity?
5. Have attached parts passed a pull test after heat aging?
6. What are the carton dimensions and layer configuration for my pack — designed against crush, or just against weight?
7. Can I receive a pre-production sample in hand before tooling starts?
Bonus question, and the most telling one: "What can't you make?" Factories that claim to do everything usually do one thing badly. A serious factory knows its lane — ours is simple-to-medium 3D shapes, not ultra-detailed realistic sculpts, and we say so up front.
What we do about it
We're a TPR squeeze-toy factory, and this list is essentially our QC checklist wearing a blog post:
• Toy-grade TPR outer skins only — no PVC.
• Recovery time specified, then re-tested after heat aging.
• Sealed fills, chosen per project.
• 3D-printed prototype before tooling — you approve the shape in hand, and cover the sample and freight costs.
• And when a design is wrong for this process, we tell you before you spend money on it.
The takeaway
Your return rate is decided in the first 200 grams of compound, not the last 200 characters of your ad copy.
Send us your design. We'll tell you straight whether it's buildable as a slow-rising squeeze toy — and, more usefully, what will go wrong with it if it isn't built right.